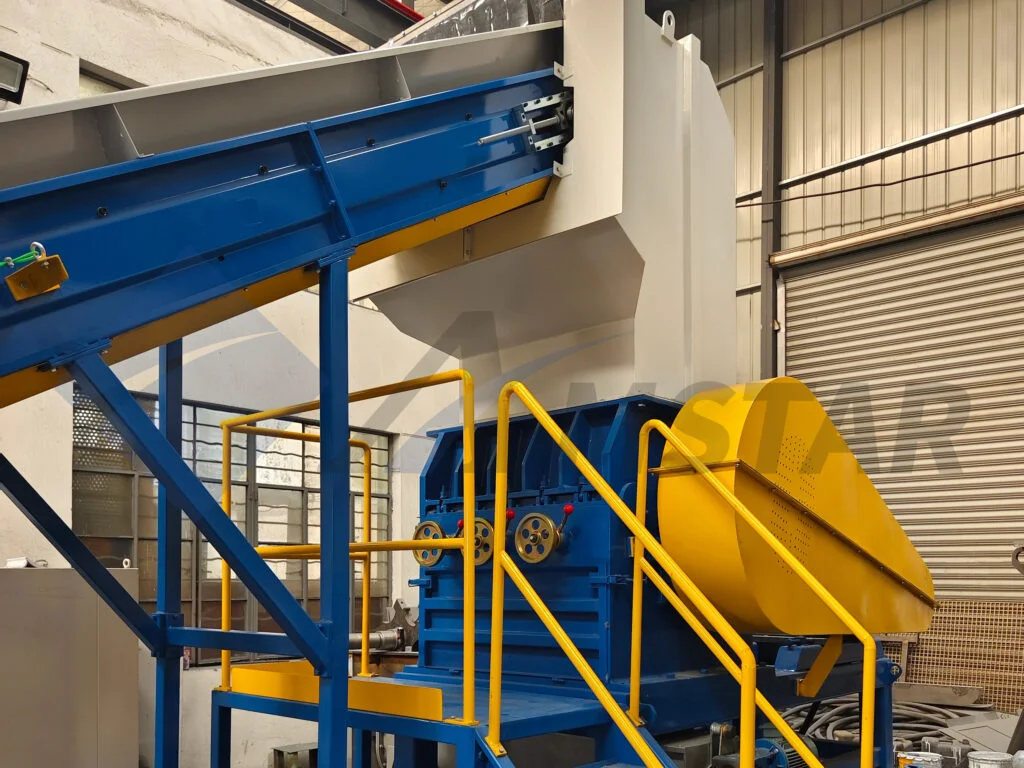
In plastic recycling, the granulator or crusher is often seen as a “basic” machine. In reality, it is one of the most influential stages in determining material quality, system stability, and downstream efficiency. Rather than viewing a plastic granulator simply as a size-reduction tool, this article looks at it from a different angle: how material behavior inside the granulator directly affects the entire recycling line.
For recyclers in North America evaluating or upgrading equipment, understanding granulation as a process-critical operation — rather than a commodity crushing step — is key to higher output, better regrind quality, and long-term line stability.
Granulation Controls Material Behavior, Not Just Size
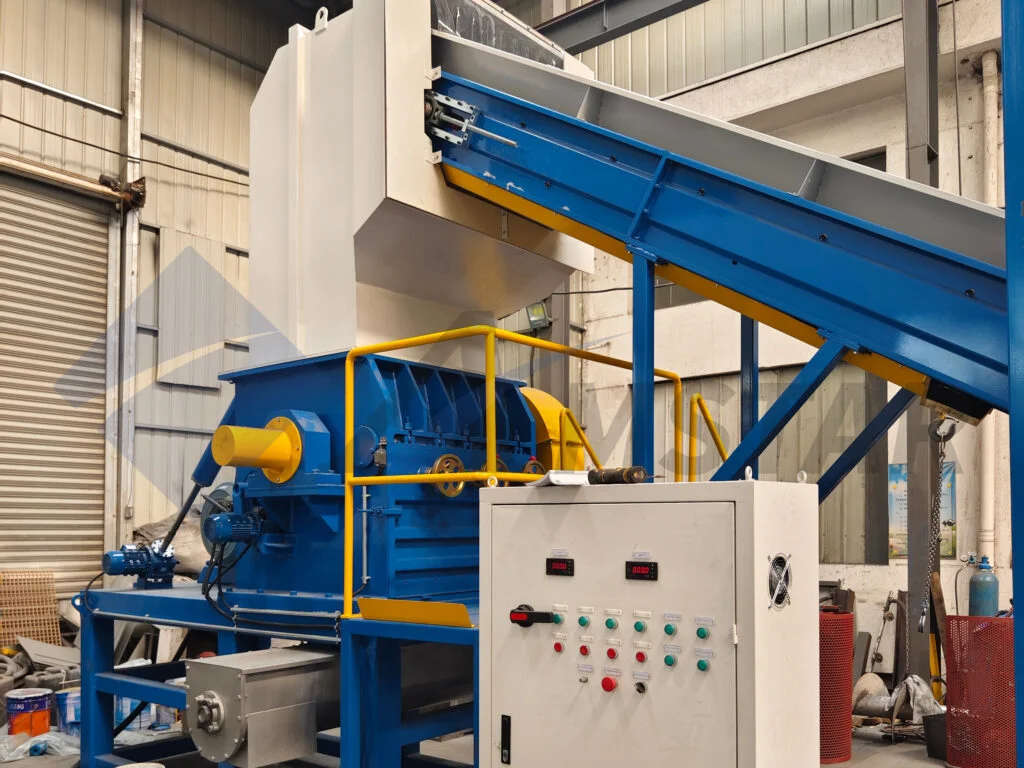
A plastic granulator does more than break plastics into smaller pieces. It controls how material behaves before washing, separation, extrusion, or pelletizing. During granulation, the machine determines particle size consistency, edge sharpness and flake geometry, heat generation during cutting, and dust and fines content.
These factors directly influence washing efficiency, drying performance, and even extrusion stability later in the process. In other words, poor granulation cannot be “fixed” downstream — whatever the granulator gets wrong, the rest of the line has to live with.
How Material Type Changes Granulator Performance
Different plastics react very differently inside a crusher or granulator.
| Material Type | Granulation Behavior | Key Consideration |
| Rigid PP / HDPE | Clean cutting, stable load | Rotor speed & knife gap |
| PET bottles | Brittle, sharp flakes | Screen size & wear resistance |
| Film (LDPE/LLDPE) | Wrapping tendency | Rotor design & feeding control |
| Injection scrap | Dense & thick | Motor torque & blade strength |
A well-designed plastic granulator adapts to material behavior, not just material type. That is why lines built around specific feedstocks — from rigid HDPE and PP recycling lines to PET bottle systems — pair the granulator configuration with everything downstream of it.
Blade Design: The Heart of Cutting Quality
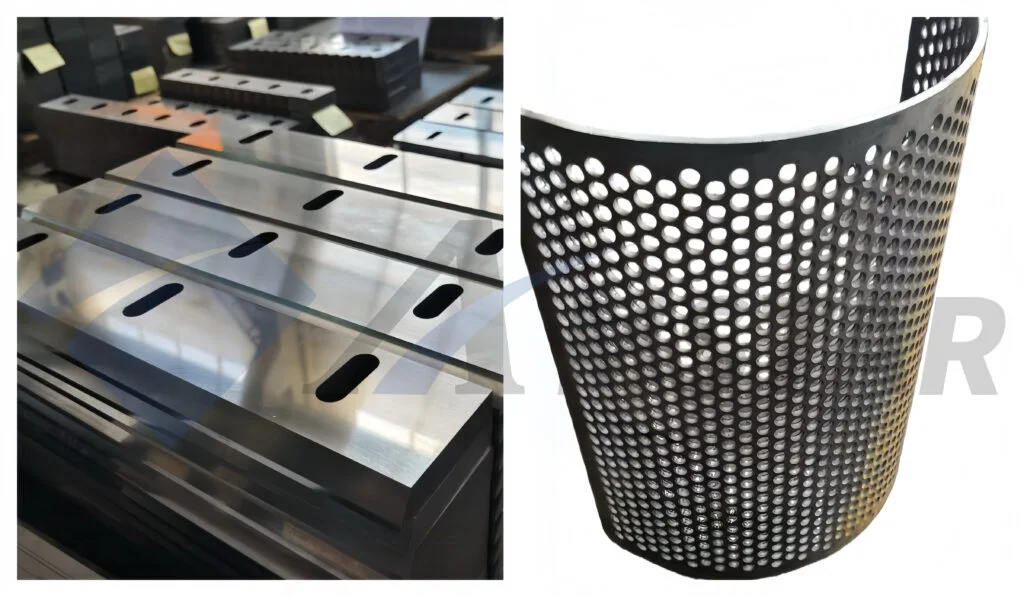
While motors and frames matter, knife geometry defines cutting quality. Cutting angle affects power draw and heat buildup; knife arrangement — staggered versus straight alignment — influences throughput and uniformity; stable clearance control keeps particle size consistent with low dust; and blade material hardness balances wear life against cutting sharpness.
A stable blade system produces uniform regrind, reduces vibration, and extends maintenance intervals. This is why industrial plastic granulators are engineered for their application, not bought as standardized commodities.
Screen Size as a Process Decision
Many buyers select screen size based only on output size. In practice, screen selection should be based on what happens next: washing lines favor larger, open flakes that improve friction washing; pelletizing needs consistent size to avoid feeding fluctuation; agglomeration or densifying cares more about controlled thickness than length.
Choosing the wrong screen increases fines, energy use, and wear across the entire line. When in doubt, test with your actual material — screen performance varies far more with feedstock behavior than catalog tables suggest.
Granulator Stability and Line Efficiency
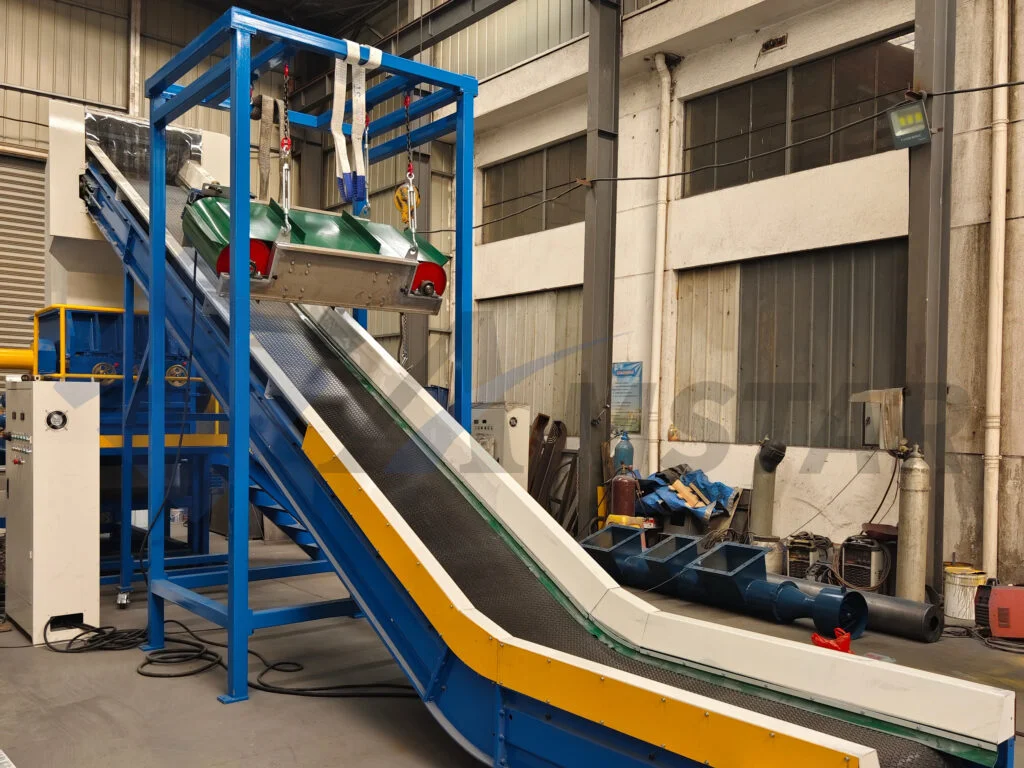
In a complete recycling system, the granulator is often the first high-load machine. If it runs unstably, the entire line suffers: conveyors overload, washing tanks fluctuate, dryers run imbalanced, and extruders feed inconsistently.
A properly sized plastic crusher with stable cutting behavior becomes a buffer, not a bottleneck. Evenly granulated material also dewaters more predictably — a real advantage before a centrifugal dewatering machine, where uniform particle size translates directly into consistent residual moisture.
Selecting a Granulator from a System Perspective
Instead of asking “How many kilograms per hour?”, the better questions are: What material behavior do I need after crushing? How stable must particle size be for my downstream equipment? Is my process more sensitive to fines, heat, or shape?
When a plastic granulator is selected as part of a system, not as a standalone machine, the entire recycling line becomes easier to operate, maintain, and scale.
Maintenance Tips for Plastic Granulators
Granulator maintenance is mostly about the cutting chamber. Rotate or replace knives before they go fully dull — dull knives generate heat, fines, and higher power draw long before output visibly degrades. Always re-check knife gap after a blade change; even a fraction of a millimeter of extra clearance increases fines. Inspect screens for wear, blinding, and cracked welds, and watch bearing temperature and belt condition. Tracking motor amperage over time is the simplest early-warning system you have: a slow upward creep almost always means the knives need attention.
A plastic granulator or crusher is not just the first step in recycling — it quietly defines everything that follows. Understanding material behavior inside the granulator is the key to higher output, better quality regrind, and long-term system stability. In modern plastic recycling plants, granulation is no longer a simple crushing task, but a process-critical operation.
Frequently Asked Questions
What is the difference between a plastic granulator and a shredder?
A granulator is a high-speed cutting machine that produces fine, uniform regrind, while a shredder is a low-speed, high-torque machine that tears bulky material into coarse pieces. In a typical line the shredder comes first for volume control, and the granulator follows to finish the size reduction with tight particle-size control.
Why does granulation quality matter so much for the whole line?
Because poor granulation cannot be fixed downstream. Oversized flakes wash poorly, excess fines clog filters and carry through drying, and heat-damaged material weakens extruded pellets. Particle size consistency, flake geometry, and fines content set at the granulator directly determine washing efficiency, drying performance, and extrusion stability.
How does material type change granulator performance?
Rigid PP and HDPE cut cleanly with stable load; PET bottles are brittle and produce sharp flakes that accelerate wear; LDPE film tends to wrap around the rotor and needs careful feeding; thick injection scrap demands high torque and strong blades. A well-designed granulator adapts to material behavior, not just material type.
What should I look for in granulator blade design?
Knife geometry defines cutting quality: cutting angle affects power draw and heat buildup, knife arrangement (staggered vs straight) influences throughput and uniformity, and tight clearance control keeps particle size stable with low dust. Harder blade steel lasts longer but must be balanced against cutting sharpness for your material mix.
How do I choose the right screen size?
Choose screen size based on what happens next, not just the output size you want. Washing lines favor larger, open flakes that friction-wash well; pelletizing needs consistent size to avoid feeding fluctuation; densifying cares more about controlled thickness than length. The wrong screen increases fines, energy use, and wear across the entire line.
Wet or dry granulation — which is better?
Wet granulation sprays water during cutting, which cools the knives, suppresses dust, and starts the washing process early — ideal for dirty post-consumer material heading into a film washing line or PET washing line. Dry granulation suits clean in-house scrap where water would only add a drying step. Many full PET bottle recycling lines use wet granulation for exactly this reason.
How do I reduce fines and dust from my granulator?
Keep knives sharp and clearances tight, match screen size to the application, avoid over-feeding, and consider wet granulation for dusty materials. Excess fines usually signal dull blades, an oversized screen, or a rotor speed that does not suit the material — all fixable without replacing the machine.
What maintenance does a plastic granulator need?
Rotate or replace knives on schedule, verify knife gap after every change, inspect screens for wear and blinding, check bearings and belts, and monitor power draw as an early warning of dull blades. A granulator running with sharp knives and correct clearances uses less energy and produces far more uniform regrind.
Can one granulator handle both rigid plastics and film?
It can, but not optimally. Film needs an anti-wrapping rotor design and controlled feeding, while rigid scrap needs torque and cutting force. Plants running both usually dedicate machines or at least swap rotors and screens. For high volumes of film, a purpose-built film shredding and densifying line is far more efficient than forcing film through a rigid-plastic granulator.
Inquiries
To learn more about this product, please send us a message using the form below: